Fraunhofer ILT and MacLean-Fogg have jointly produced a complex injection moulded tool inlay using Laser Powder Bed Fusion (PBF-LB/M). The specially developed L-40 tool steel enables for the first time the printing of high-volume, heavily loaded tools and thus the implementation of conformal cooling. This is a major step forward in additive manufacturing.
The automotive industry is in the midst of profound change. Cost pressures and the transition to electric driving are forcing many manufacturers to fundamentally rethink their vehicle architectures and production processes. Many manufacturers are aiming for as few but highly complex structural components as possible. Especially for large aluminium components, such as frame or transmission parts, this also places higher demands on the tools. They must be thermally highly loadable, allow for variants and be adaptable to new geometries as quickly as possible.
New challenges
This change brings new challenges. The moulds required must not only be larger than before, but also more resistant, with complex geometries and shorter development times. This is exactly where a project by the Fraunhofer-Institut für Lasertechnik ILT, together with L-40 powder manufacturer MacLean-Fogg and Toyota as end-user, comes in.
Additive manufacturing
By using a PBF-LB/M machine developed at the Fraunhofer ILT based on a gantry with a scalable build volume and the additive manufacturing tool steel developed by MacLean-Fogg, very large injection moulds with contour cooling additive could be manufactured for the first time - suitable for large-volume high-pressure injection moulding components (HPDC).
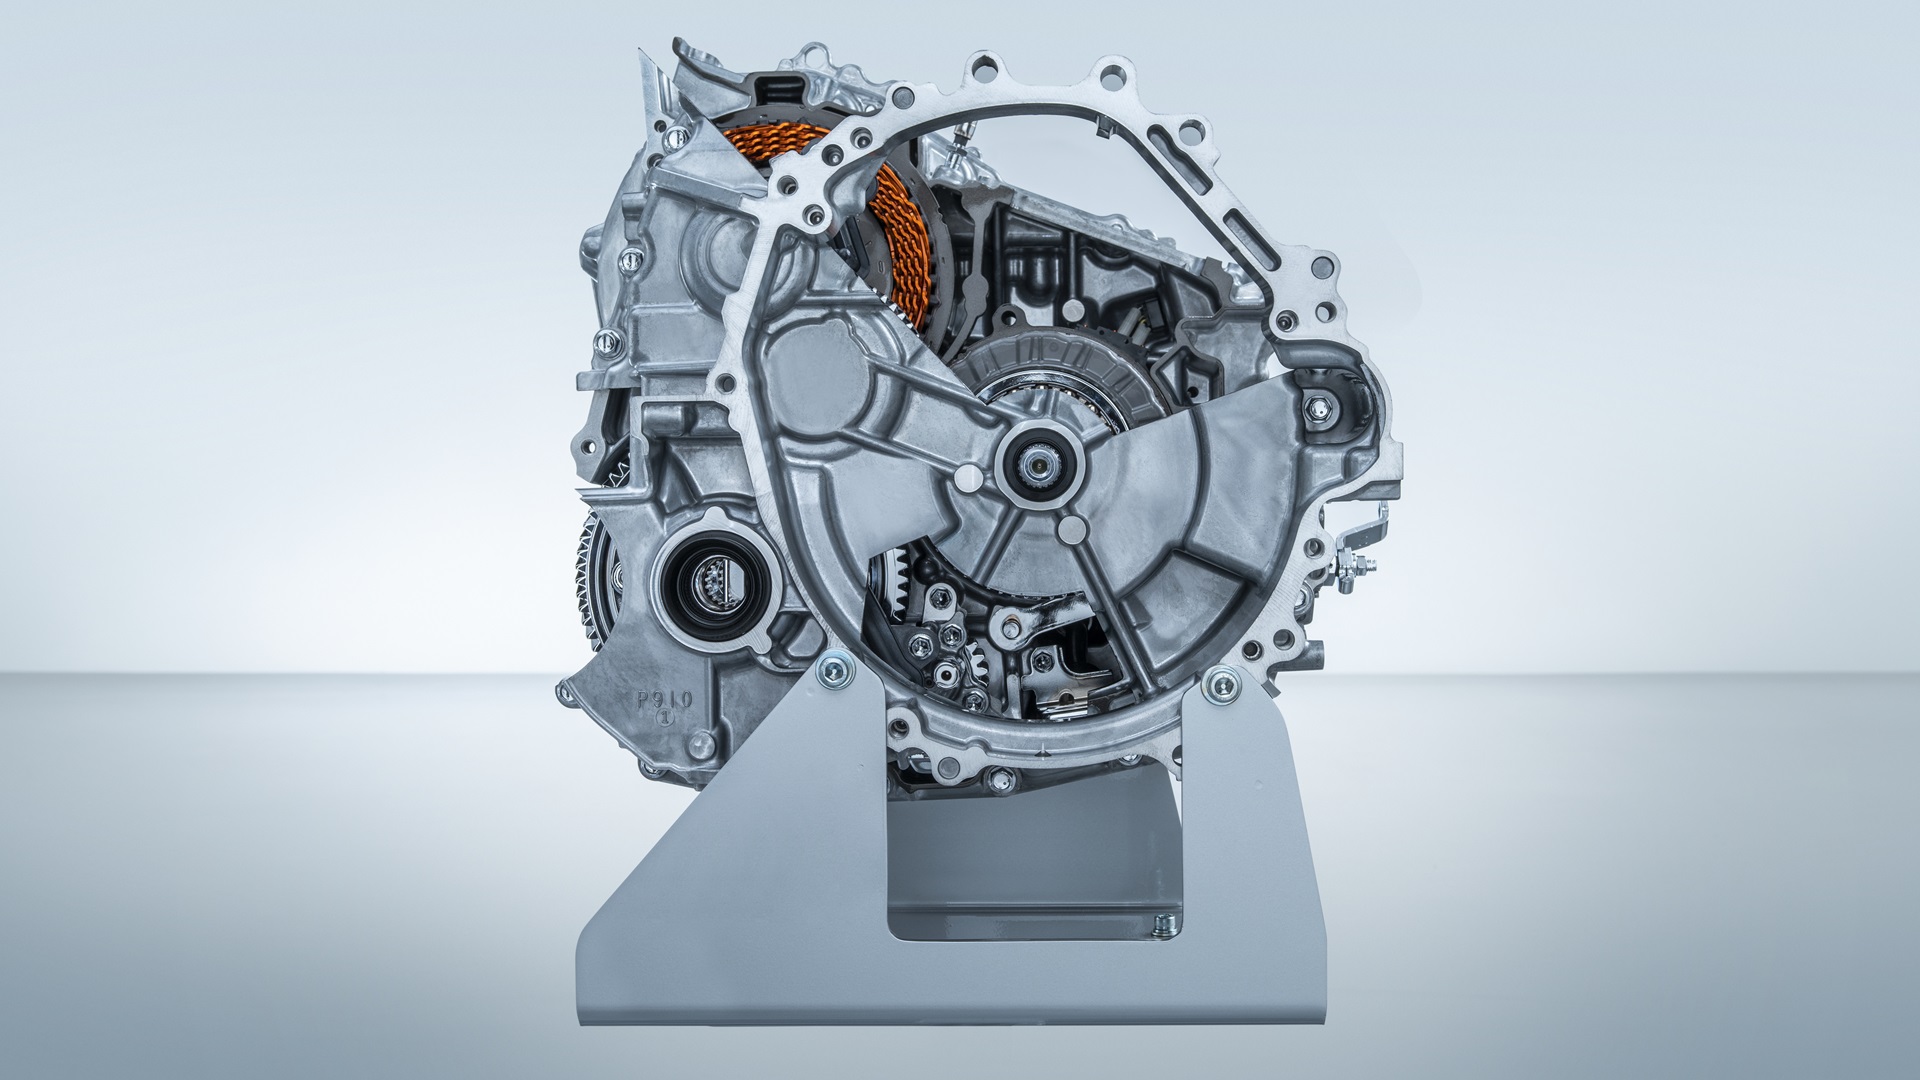
The aluminium die-casting tool, manufactured via additive manufacturing, is part of the tooling for the transmission housing of the Toyota Yaris hybrid car. It was chosen because of its size and soldering challenges and high maintenance time. (Photo: Toyota Europe)
Solid geometries
As large casting processes become more common, the demands on tools increase. The moulds must repeatedly maintain accurate component quality at very large numbers and withstand extreme mechanical and thermal loads. To ensure a sufficient lifetime of tool inserts, complex, internal cooling structures are required, which cannot be made with conventional manufacturing processes.
Available build volume and steels
Two main problems have so far limited the possibilities of applying additive manufacturing to such large injection moulds. First, the available build volume of classic PBF-LB/M machines is too small to produce mould or die inserts with dimensions of 600 x 600 mm² or more in one piece. Secondly, the tool steels used so far - in particular H11 (1.2343), H13 (1.2344) or M300 - cannot be processed reliably in this size range (> 20,000 cm³). Even with optimum parameters, there is a risk of cracking, thermal deformation and insufficient mechanical properties.
This is true both during laser-based build and during subsequent heat treatment. The greater the temperature gradients within the part during the manufacturing process, the greater the risk - an effect that is particularly noticeable with large workpieces.
New machines and materials
"To overcome these limitations, we need a new generation of machines and materials specifically tailored to the requirements of large-volume tools," explains Niklas Prätzsch, group leader LPBF process technology at Fraunhofer ILT. "Precisely this combination was the subject of the latest changes we made."
The new material and machine technology makes it possible for the first time to produce large tools with a free-form cooling structure. This not only allows targeted reduction of local temperature peaks in the casting process, but also increases the number of variants and extends service life at the same time. This means that different components can be produced on one tool platform without having to produce new tools each time.
Production of large components without cracks
The PBF-LB/M machine with 5 lasers and gantry construction developed at Fraunhofer ILT, with a current build volume of 1,000 x 800 x 350 mm³, has been further developed for this purpose. Unlike conventional systems, this machine has a movable processing head and local protective gas guidance, so that the build volume can be scaled linearly along the machine axes with the same process boundary conditions (protective gas flow rate, laser beam deflection angle, etc.). This means that additive manufacturing of even larger tools will be possible in the future.
Temperature
A heatable substrate module was also developed to minimise the temperature gradients crucial for high-volume tools. The build platform now reaches a temperature of 200 °C. This means that each new layer does not cool to room temperature, but only to a predetermined thermal plateau. This approach reduces thermally induced stresses and the risk of cracking during the construction process. The combination of a large installation space, high process stability and active preheating makes this system one of the world's first LPBF systems suitable for economical production of near-net-shape injection moulds, even for mega- or gigagites.
L-40 material
"The key to success lies in MacLean-Fogg's L-40 material, which is tailored to the requirements of PBF-LB/M," says Prätzsch. This steel is characterised by a significantly reduced tendency to crack compared to conventional tool steels - both during production and heat treatment. Extensive tests have successfully validated both the parameter transfer to the new machine concept and its performance in complex geometries - e.g. with round or overhanging cooling channels. Initial applications show that the lifetime of tools produced in this way can be significantly extended compared to conventional moulds.
Hybrid manufacturing for serial tools
As part of the project, the partners produced a tooling insert for a gearbox housing already in use at Toyota. The injection-moulded insert contains a complex network of cooling channels. That in itself is a clear advantage of additive manufacturing that could not be achieved with conventional machining. To design the printed tool, the project team chose a hybrid process on a specially manufactured preform that already had vertical cooling channels. The precise positioning and reliable connection of the two components placed high demands on machine calibration, precision and process control. Such hybrid structures have the potential to further reduce build time and costs, as the process is used only in those component areas where conventional processes do not work.
Complex cooling structure
The researchers designed the complex cooling structure so that critical areas of the mould are effectively tempered during the injection moulding process. This reduces thermal stress, which significantly extends the life of the mould. In previous projects, a similar printed mould already had a lifetime up to four times longer than a conventional H13 mould. After the mould insert was built, it was stress-annealed and the functional surfaces were conventionally milled. The high dimensional accuracy of the printed base body required only precise final finishing without additional material feeding.
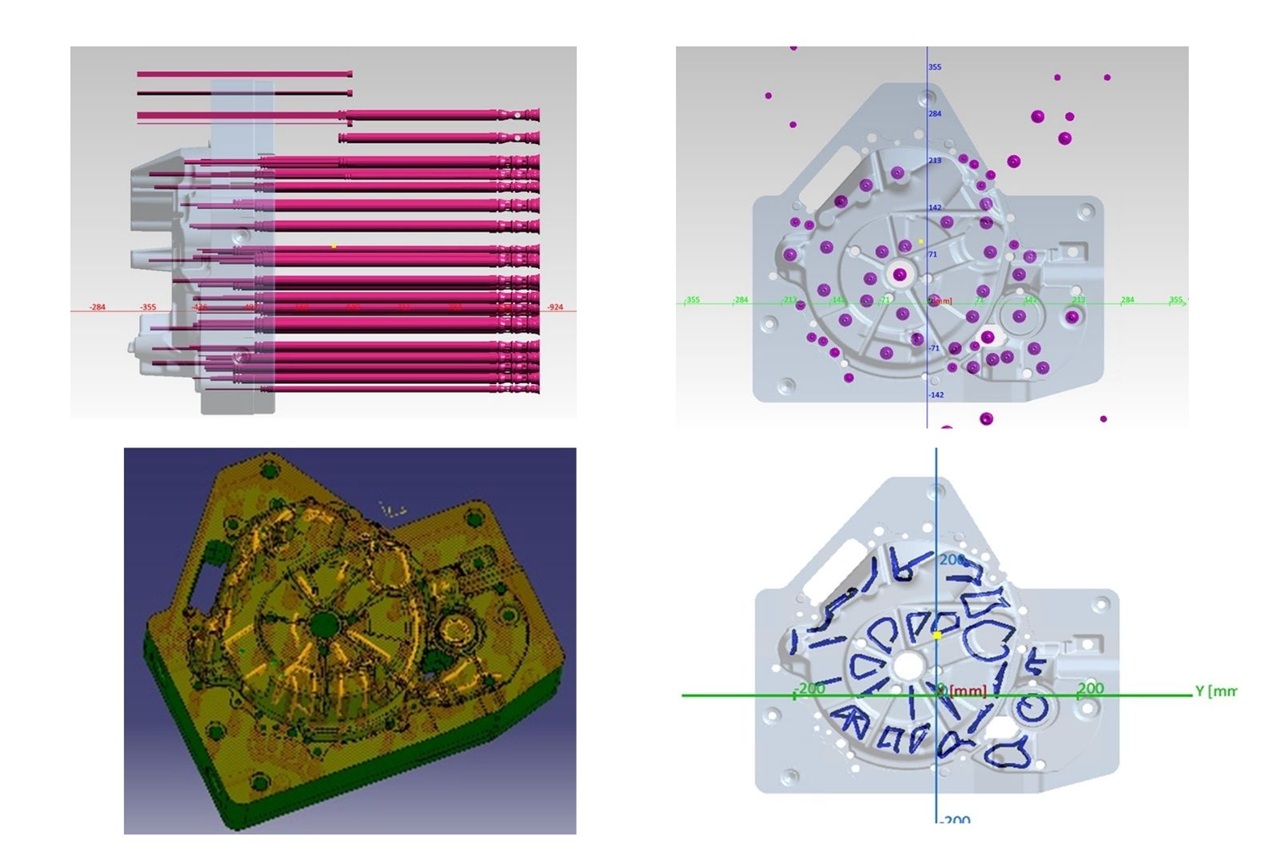
Design of the cooling channels. (Photo: MacLean Additive)
Towards efficient and durable moulds in the automotive industry
The production of large-format moulds using additive manufacturing provides an answer to several key challenges in today's automotive production, especially in the context of the transformation to electric driving. A decisive advantage is conformal cooling, which for the first time can be freely designed using 3D printing. The cooling channels can be optimally adapted to the thermally stressed areas of the tool. This lowers local temperature peaks, reduces thermomechanical wear and significantly extends the life of the mould.
More advantages of additive manufacturing
At the same time, additive manufacturing offers the possibility of drastically reducing lead times. For OEMs, this means shorter development cycles and faster time-to-market for new vehicle platforms. The ability to build large numbers of tools using hybrid technology creates additional flexibility. Components with defined interfaces can be efficiently added and functionally optimised without having to produce the whole part from scratch. This reduces both material consumption and cost per tool.
Toyota
For car manufacturers like Toyota, which are constantly striving for flexible production and rely on fewer individual parts and more complex structures, these developments open up new possibilities in tooling strategy. It offers less effort in tool production, longer lead times and the ability to realise multiple variants with just one tool.
Plastic
However, the potential extends far beyond the individual case: the developed process chain is suitable not only for large aluminium HPDC tool changers, but also for applications in plastics processing or in the field of composite materials. Wherever heavily loaded tools with complex cooling and limited batch sizes are required, additive manufacturing can offer clear advantages.
Source: Fraunhofer ILT
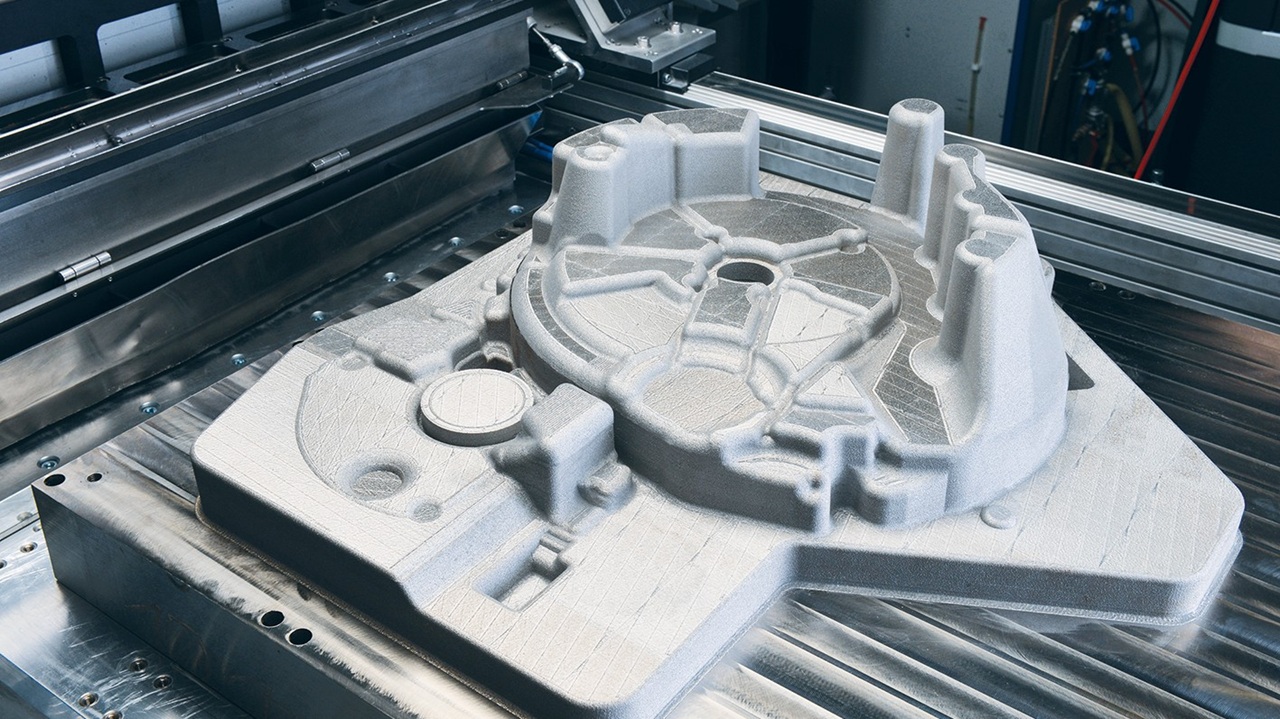
Opening photo: Injection moulded tool insert made of tool steel L-40, produced by additive manufacturing. The large volumetric mould was produced at Fraunhofer ILT using laser powder melting with conformal cooling. (Photo: Fraunhofer ILT, Aachen, Germany)
Read more about additive manufacturing: Manifesto: make the EU a world leader in additive manufacturing